Description
Key Technical Specifications
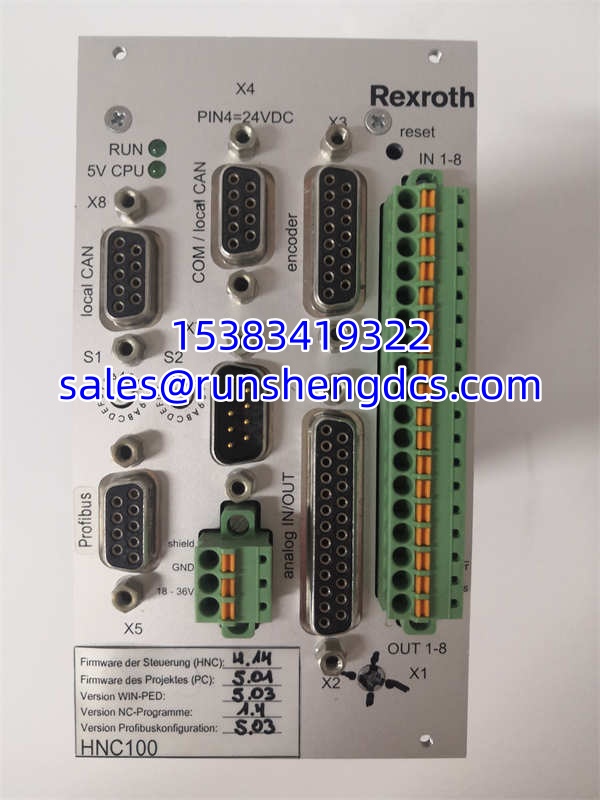
- Product Type: Digital axis controller
- Series: Rexroth VT-HNC100
- Order Number: R900958999
- Model Interpretation: VT-HNC100-1-2X/W-08-P-0
- Hydraulic Variant: 1 hydraulic axis
- Component Series: 2X — your unit shows 23
- Housing: Wall-mount
- Digital I/O: 8 digital inputs/outputs
- Bus Connection: PROFIBUS DP
- Supply Voltage: Typically 24 V DC range, commonly 18–36 V DC for HNC100 family
- Typical Use: Position, pressure/force, speed, or basic monitoring control of hydraulic drives
- Commissioning: PC-based service/parameter software via service interface
Product Introduction
A hydraulic press, test rig, or rolling-mill screw-down system does not care that a PLC is sending a reference. It cares whether the valve gets the right command, whether the feedback is stable, and whether the controller can hold position when oil temperature, load, and pressure start moving. The Rexroth VT-HNC100-1-23W-08-P-0 / R900958999 sits between the plant control system and the hydraulic valve, closing the loop on one hydraulic axis.
This unit is used where proportional or servo valves need precise digital control rather than raw analog wiring. It handles reference inputs, feedback conditioning, PID-type closed-loop control, diagnostics, and bus communication. In practice, it is the kind of board you replace when the axis drifts, faults repeatedly, loses PROFIBUS, or no longer holds position — not when you simply need another PLC digital output card.
Troubleshooting Quick Reference
| Fault | Likely Cause | Quick Check | Fix |
|---|---|---|---|
| Axis will not move | No 24 V supply, enable missing, or valve drive fault | Measure supply at controller terminals; check 8 digital I/O status | Confirm 24 V DC, enable signal, and valve command output |
| Position drift | Feedback sensor, LVDT, wiring, or PID issue | Check analog feedback and reference signals | Inspect sensor wiring, shielding, and controller parameters |
| PROFIBUS fault | Bus address, cable, termination, or node conflict | Check PROFIBUS LED status and bus address | Verify address, termination, cable, and PLC node config |
| Controller not recognized | Wrong order code or firmware mismatch | Read nameplate: VT-HNC100-1-2X/W-08-P-0 and R900958999 | Replace with exact order code or confirm parameter set |
| Erratic valve output | EMI, bad ground, or damaged analog stage | Check shielding, ground, and analog output | Separate signal cables from power cables; check valve coil |
| Frequent alarms | Parameter loss, sensor fault, or hydraulic fault | Read diagnostic via service software | Back up parameters; verify sensor and hydraulic hardware |
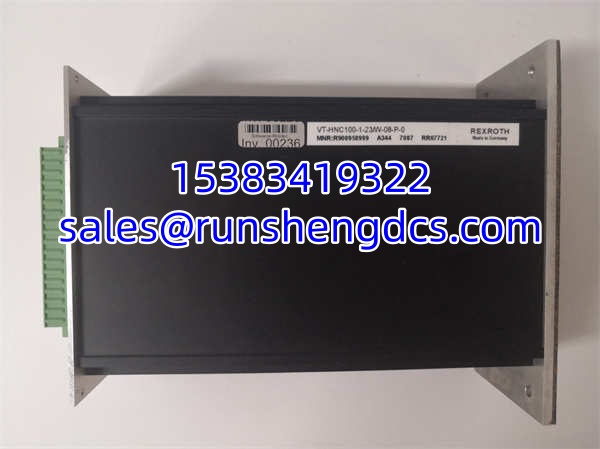
VT-HNC100-1-23W-08-P-0 R900958999
Application Scenarios & Pain Points
- Hydraulic presses: Position and force control must stay repeatable across cycles. The pain is drift caused by oil temperature, valve hysteresis, or lost feedback.
- Rolling mills / metal forming: Screw-down or gap control needs tight closed-loop stability. A failed axis controller can scrap product or force a line stop.
- Test benches: Repeatable pressure/force profiles are required. The bottleneck is often parameter integrity, not the valve itself.
- Injection molding or hydraulic automation: Proportional valve control must match machine cycle timing. PROFIBUS faults here look like PLC problems until you check the axis controller.
- Machine tool hydraulic clamping or positioning: Intermittent axis faults are often blamed on the PLC, but the real cause can be feedback wiring or a degraded module.